
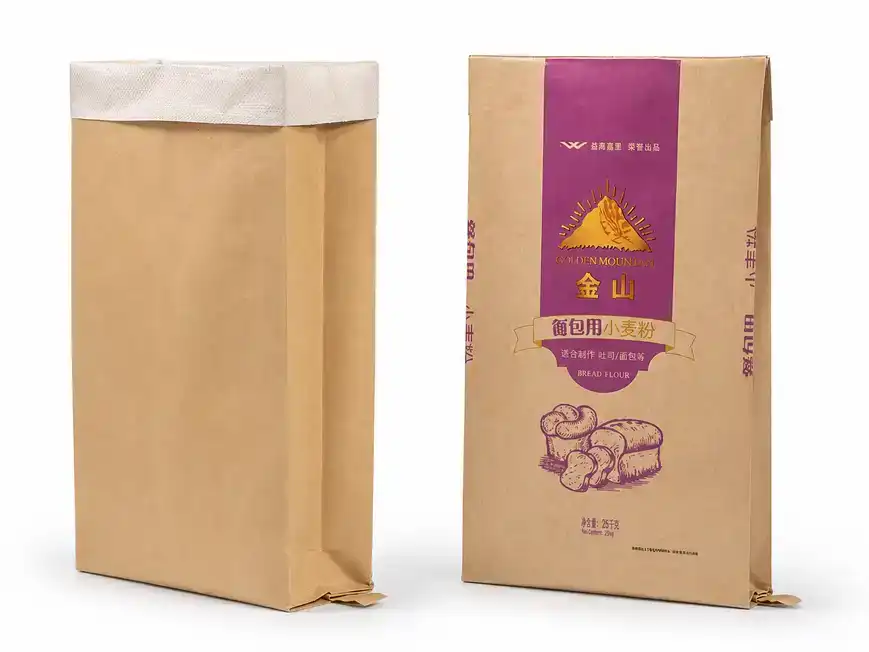
VIDEPAK Kraft Paper Laminated Woven Bags: Strength, Print Value, and Supply-Chain Confidence in One Package
Industrial packaging has a difficult job. It must protect a product, move smoothly through a filling line, survive warehouses and long-distance transport, communicate a brand, and still support realistic cost and sustainability goals. A bag that performs only one of these jobs may look acceptable in a sample room yet fail in the real supply chain. VIDEPAK develops Kraft Paper Laminated Woven Bags to bring these needs together through a practical composite structure: a printable kraft paper surface outside, a load-bearing polypropylene woven fabric inside, and a controlled bonding layer between them. The result is not simply paper added to plastic. It is a packaging system in which each layer has a clear task and each task supports the next.
Key idea: The value of Kraft Paper Laminated Woven Bags is not measured only by bag price. It is measured by the combination of filling efficiency, reduced breakage risk, clear printing, stable pallet handling, product protection, and consistent supply.
The Hybrid Packaging Advantage
Kraft Paper Laminated Woven Bags occupy a useful position between traditional paper sacks and plain woven polypropylene sacks. Paper gives a familiar natural look, a good writing and printing surface, and useful friction for stacking. Woven polypropylene gives tensile strength, tear resistance, shape retention, and efficient material use. When these materials are joined in a carefully designed structure, buyers gain the visual quality of paper without asking paper alone to carry every mechanical load, and they gain the strength of woven fabric without accepting a basic industrial appearance. The original VIDEPAK product concept is built on this balanced “division of labor,” and modern sack-paper guidance also confirms that paper properties such as porosity, stretch, tensile energy absorption, surface condition, and moisture response directly affect filling and bag performance.
This balance matters because packaging failure rarely begins with one dramatic event. It begins with a weak corner, a poorly bonded area, a seam that carries too much stress, an outer surface that scuffs, or a barrier level that does not match the product. One small weakness becomes product leakage; leakage becomes dust, rework, claims, and lost confidence. VIDEPAK therefore treats Kraft Paper Laminated Woven Bags as an engineered package rather than a decorated commodity bag. Strong inside, clear outside. Flexible in design, disciplined in production. Simple to use, difficult to replace once it proves its value.
Mechanical Support
The woven PP body carries the load, resists tearing, and helps the package retain its form during filling, stacking, and transport.
Brand Communication
The kraft paper face creates a clean area for logos, product information, barcodes, handling marks, and market-specific text.
Barrier Flexibility
Coatings, liners, and controlled venting can be selected to manage moisture, fine powder, grease, air release, or odor needs.
Operational Fit
Open-mouth, sewn, pinch-bottom, and valve-style options allow the package to match different fillers and end-user habits.
VIDEPAK’s wider Laminated Woven Bags range follows the same engineering logic, although the visible outer layer can change. Some projects focus on kraft paper for a natural and industrial look; others use printed film for sharper graphics or stronger surface moisture resistance. The common foundation is a woven structure combined with a functional outer or inner layer. This makes Laminated Woven Bags a platform rather than one fixed product. Size, weight, closure, print, coefficient of friction, perforation, liner, and barrier can all be discussed as connected choices. Good packaging does not ask, “How many options can we add?” It asks, “Which options remove the customer’s real risk?”
Product Structure and Practical Parameters
Layer-by-Layer Engineering
The outer kraft paper layer of Kraft Paper Laminated Woven Bags provides more than appearance. Its basis weight, fiber strength, porosity, stretch, water absorption, friction, smoothness, and print surface can influence converting, filling, stacking, and brand presentation. High tensile strength alone is not enough. Sack-paper engineering places strong emphasis on tensile energy absorption, which combines strength and stretch and relates to how the paper wall handles impact during drop events. Porosity is equally important for powdered products because trapped filling air must leave the package without carrying valuable product into the work area. High-porosity paper can support faster filling, smaller filled volume, and a cleaner process when the total bag design is properly vented.
The inner woven PP fabric is the structural skeleton. Polypropylene resin is converted into oriented tapes, and those tapes are woven in warp and weft directions to distribute load across the bag body. Fabric weight, tape denier, weave density, width control, and coating uniformity must work together. A heavier fabric is not automatically the best fabric, just as thicker paper is not automatically the best paper. Over-specification adds cost and stiffness; under-specification raises the chance of seam stress, puncture, deformation, or breakage. VIDEPAK develops the structure around the filled weight, bulk density, particle shape, drop height, pallet pattern, climate, transport route, and customer equipment.
The lamination interface is the hinge between the paper and woven layers. Its purpose is to create stable bonding while controlling stiffness, flatness, print behavior, and resistance to local separation. Depending on the project, the package may also include an internal PE liner, a free film, a moisture-control coating, micro-perforation, anti-slip treatment, or easy-open tape. Each addition must have a reason. A liner can improve powder retention and moisture protection, but it can also affect air release. More lamination can improve barrier, but it can also add material complexity. The best Kraft Paper Laminated Woven Bags are therefore not the bags with the most layers; they are the bags with the right layers.
The ranges above are practical starting points, not automatic promises. VIDEPAK’s published product information identifies 10–50 kg as a common capacity range and lists several standard conversion styles, while sack-paper references describe natural or white papers, porosity classes, wet-strength choices, coatings, and print-oriented surfaces. Final values must be confirmed through the customer’s product data and trials because a 25 kg bag of dense mineral powder behaves very differently from a 25 kg bag of light feed pellets. Same weight, different force. Same dimensions, different air. Same route, different risk.
Printing deserves its own engineering review because the paper surface carries both brand value and operating data. Natural brown kraft creates a warm, direct look and can make dark, strong colors highly visible; white kraft gives a cleaner base when the artwork uses pale colors, fine screens, or detailed product images. Print performance also depends on paper formation, surface roughness, ink system, drying, coverage, and the amount of movement allowed by the underlying fabric. A good artwork file cannot correct an unstable substrate, and a good substrate cannot correct weak prepress control. VIDEPAK therefore recommends confirming color targets, text size, barcode position, print direction, seam location, and the relationship between artwork panels before production. The bag must look right when flat, when filled, and when stacked.
Closure design is equally visible in daily use. A sewn open mouth offers broad equipment compatibility and a familiar industrial format. A pinch-bottom design can produce a clean, sealed appearance when the filling and closing system is suitable. A valve structure can support fast powder filling and a compact filled shape, but valve size, position, sleeve material, deaeration, and sealing method must match the filler and product. Easy-open tape can improve user convenience, while an internal liner may need to be cuffed, heat sealed, tied, or integrated in another way. These details appear small on a drawing. On the packing line, they decide speed. In the warehouse, they decide stability. At the customer site, they decide whether the package opens cleanly or becomes a source of waste and frustration.
Specification Rule
Do not select Kraft Paper Laminated Woven Bags by filled weight alone. Share bulk density, particle size, moisture sensitivity, filling temperature, fill rate, drop height, storage climate, pallet pattern, transport distance, and opening method. These details turn a quotation into an engineering decision.
Manufacturing Workflow and Quality Control
From Raw Material to Finished Bag
Reliable Laminated Woven Bags come from a controlled chain, not from one final inspection. The chain begins with resin and paper verification, continues through tape extrusion, winding, circular weaving, lamination, printing, cutting, forming, sewing or sealing, and ends with finished-bag testing and shipment release. Every stage affects the next. Unstable tape width can produce uneven fabric. Uneven fabric can reduce lamination consistency. Poor lamination can affect paper flatness and print. Inaccurate cutting can move the seam into a high-stress area. Quality is cumulative; so is failure.
At the resin stage, incoming material should be checked against agreed identity and performance requirements. During extrusion, operators control melt behavior, tape width, draw ratio, and winding. During weaving, the team monitors weave density, fabric width, appearance, and defects. During lamination, bond stability, coating distribution, temperature, tension, and surface flatness become critical. Printing adds another group of controls: artwork version, color, registration, text clarity, barcode quality, and drying. Conversion then brings dimensions, valve geometry, bottom fold, thread, stitch density, sealing, easy-open systems, and bundle count into the quality plan.
VIDEPAK states that it was founded in 2008, operates with more than 500 employees, uses over 100 circular looms, 16 extrusion lines, and more than 30 lamination and printing machines, and supplies customers in over 70 countries. The company also reports production and testing aligned with ISO, ASTM, EN, and JIS frameworks, supported by incoming-material checks and batch testing such as impact, tensile, and weather-resistance evaluation. These published capabilities matter not as decoration, but because scale, equipment depth, and a documented quality system help a Manufacturer manage repeat orders, multiple specifications, and export schedules with greater control.
Testing should be selected by function. Paper grammage can be checked under ISO 536; paper tensile, stretch, and tensile energy absorption under ISO 1924-3; water absorption through the Cobb method under ISO 535; and thin-film tensile or impact behavior through relevant ASTM film methods. A finished bag still needs application-level validation because a strong paper sheet and a strong fabric do not automatically guarantee a strong seam, a stable valve, or a safe pallet. Material tests explain components. Filled-bag trials explain the package.
Approval discipline protects both sides of the supply relationship. The approved specification should identify every critical item in language that purchasing, production, quality, and sales teams can understand: nominal and tolerance dimensions, paper identity, fabric construction, laminate structure, print colors, artwork revision, closure details, liner features, packing quantity, pallet or bale method, and required tests. When changes are needed, they should be reviewed as controlled revisions rather than informal production notes. This prevents an artwork correction from accidentally changing the bag size, or a material substitution from changing filling behavior. Clear records are not paperwork for its own sake. They are the bridge between a successful sample and a successful repeat order.
Quality release should also reflect the order’s risk level. A routine dry-granule bag may require a focused set of dimensional, appearance, seam, and drop checks. A moisture-sensitive powder may require additional liner, seal, or barrier evaluation. A food-related project may need documented material declarations and hygiene controls agreed for the target market. An outdoor application may need weathering or UV-related review. VIDEPAK can organize these requirements in an inspection plan so the test burden remains proportional: enough evidence to protect the customer, without adding tests that do not improve the decision.
Applications, Performance, and Selection Logic
Matching the Bag to Product Risk
Kraft Paper Laminated Woven Bags are well suited to dry products that need both mechanical support and strong communication on the package. Common project areas include food ingredients, flour, starch, milk powder, animal feed, pet food, seeds, fertilizers, chemicals, minerals, cement-related materials, and other powders or granules. Yet an application name is only the beginning. Flour and mineral powder are both powders, but their hygiene, abrasion, density, venting, and moisture needs differ. Feed pellets and fertilizer granules are both free-flowing, but their edges, odors, chemical behavior, and storage conditions differ. The design must follow the product, not the category label. Industry sack guidance recognizes these broad application families and explains that paper sacks may add polymers or films to achieve moisture, oxygen, grease, or other barrier functions.
For food and feed projects, the discussion should cover direct or indirect food contact, odor and migration expectations, hygiene controls, liner selection, traceability, and opening behavior. A clean kraft face can carry product instructions and batch information clearly, while the woven layer supports handling. For fertilizers and moisture-sensitive chemicals, barrier design and seam tightness move higher on the priority list. For building materials and minerals, puncture, abrasion, air release, dust control, and drop resistance become more important. For export routes, humidity cycles, container loading, pallet stability, and long storage periods can justify a stronger or more protective structure than a short domestic route.
A practical buying sequence for Kraft Paper Laminated Woven Bags
First define the product. Then define the filling line. Then define the route. Then define the end-user experience. Only after those four steps should the final material structure, dimensions, closure, printing, and testing plan be frozen. Reverse the order, and packaging becomes guesswork.
Pallet performance deserves special attention. Paper friction can support stable stacking, but printing coverage, coatings, dust, humidity, and handling can change the effective surface. Too little friction may allow bags to slide; too much friction can slow automatic handling or damage printed surfaces. Filled shape also matters. A valve bag can form a compact block when product flow and deaeration are well managed, while an open-mouth bag may offer greater flexibility for different fillers and closure systems. The best choice depends on whether the customer values line speed, dust control, easy opening, a flat retail shape, or simple equipment compatibility.
Total cost should be calculated beyond the unit quotation. Plain bags may appear cheaper, but a buyer also pays for damaged goods, line stoppage, manual rework, cleaning, pallet failure, unreadable codes, extra labels, customer complaints, and emergency replacement orders. Laminated Woven Bags can justify their added material and converting cost when they reduce these hidden losses. The comparison should be honest: all-paper structures may offer a stronger fiber identity, while mono-material PP structures can support a simpler plastic recycling route. Composite structures provide a powerful balance of paper appearance and woven strength, but their end-of-life path depends on local collection and the exact material design.
Sustainability claims must therefore be specific. The kraft layer is fiber based; the PP layer is lightweight and durable; both can have established recycling routes when separated or managed in suitable systems. Once bonded together, however, the package is a composite, and recyclability becomes dependent on design, sorting, mill capability, contamination, and local infrastructure. Industry design-for-recyclability guidance recommends minimizing non-target material, optimizing adhesives to the minimum needed for function, and considering how coatings, films, handles, labels, and other components affect sorting and pulping. VIDEPAK can support customers in reducing unnecessary material while still protecting the packed product, because preventing product loss is also a major part of responsible packaging.
VIDEPAK as Your Long-Term Manufacturer
A capable Manufacturer does more than reproduce a drawing. It asks why the drawing exists. VIDEPAK approaches Kraft Paper Laminated Woven Bags through product analysis, specification development, sample confirmation, production control, and delivery planning. The customer may begin with an existing bag, a target filled weight, or a packaging problem. VIDEPAK’s role is to turn that starting point into measurable choices: paper grade, fabric structure, lamination, dimensions, closure, venting, liner, print, bundle method, test criteria, and order plan.
This consultative process is especially important when replacing another package. A direct copy can repeat the same weaknesses. A redesign can improve them. For example, a bag that breaks at the seam may need a change in body dimensions, sewing construction, thread, fabric, or drop orientation; simply increasing overall fabric weight may add cost without removing the stress concentration. A bag that fills slowly may need better air-release design rather than a thinner wall. A bag that slides on pallets may need a surface or filled-shape adjustment rather than stronger stretch film. The right Manufacturer looks for the root cause, not the easiest material upgrade.
Discovery
Review product data, current bag, filling equipment, route, market, and performance concerns.
Engineering
Build a balanced structure and define tolerances, artwork, closure, and validation needs.
Confirmation
Use reference samples or custom mock-ups to verify material, dimensions, printing, and usability.
Scale-Up
Control approved specifications through mass production, batch checks, packing, and export delivery.
VIDEPAK publishes two sample paths: reference samples from available stock for a quick material and print review, and custom mock-up samples made to the requested specification for detailed approval. The company lists a typical minimum order quantity of 10,000 pieces per specification for PP woven bags and kraft paper sacks, a general bulk-order lead time of 15–25 business days, and shipping options that can be planned under several common international trade terms. These are general planning figures rather than fixed promises; final timing depends on material, artwork, bag construction, testing, quantity, and production schedule.
For procurement teams, consistency is often more valuable than a dramatic sample. One perfect bag proves little if the next 100,000 bags vary in width, bond, color, or seam. VIDEPAK’s production depth and documented quality approach are designed to support repeatability across large orders. For marketing teams, the kraft surface provides a clear, useful brand area. For operations teams, the woven body and custom closure support handling. For finance teams, lower failure and rework can improve total cost. For sustainability teams, a fit-for-purpose design can reduce over-packaging and product loss. Different departments, one package. Different priorities, one controlled specification.
Build the specification around the real journey.
Kraft Paper Laminated Woven Bags combine a strong woven core, a kraft surface, flexible barrier choices, and application-focused converting. As an experienced Manufacturer, VIDEPAK supports customers from first questions to sample approval, from production control to global shipment. The objective is clear: a bag that fills well, carries safely, communicates clearly, and performs consistently from the packing line to the final user.
Expanding the Case for Kraft Paper Laminated Woven Bags
Within the broader family of Kraft Paper Woven Bags, Kraft Paper Laminated Woven Bags occupy a practical middle ground. They combine an outer kraft paper face with a woven polypropylene reinforcement layer and, when required, a tie layer, coating, or internal film. That hybrid structure is why they can deliver two benefits at once: the visual clarity, printability, and stack-friendly surface of paper on the outside, and the tensile strength, tear resistance, and shape retention of woven plastic on the inside. The supplied product page captures that hybrid idea; the deeper engineering point is that each layer performs a different job, and the package works only when those jobs are balanced rather than duplicated.
Commercially, that matters more than it first appears. kraft paper sacks can project a strong fiber-based image and perform well in many dry applications, yet they are more exposed to abrasion, humidity swings, and severe handling. Plain polypropylene woven bags are structurally efficient and widely used for dry bulk goods, but they do not always offer the same paper-like tactile quality, premium shelf presentation, or print surface that many brand owners and procurement teams want. Kraft Paper Laminated Woven Bags, therefore, often wins not by being the cheapest unit on the invoice, but by lowering total packaging cost through better print value, better handling reliability, and less product loss in transit. Not the lowest price per bag, perhaps, but often the more economical packaging system.
The sustainability argument is real, but it has to be stated without romance. The kraft paper layer may be renewable, recyclable, and food-contact suitable in the right specification; the polypropylene layer may be lightweight, chemically resistant, and compatible with established recycling loops in mono-material systems. Yet once the materials are kraft paper laminated, recyclability becomes a design issue rather than a slogan. Guidance from CEPI Eurokraft and EUROSAC is explicit: minimize non-fiber content, prefer simpler constructions, and treat two-sided laminates with caution because they are harder for conventional paper mills to process.
- VIDEPAK Kraft Paper Laminated Woven Bags: Strength, Print Value, and Supply-Chain Confidence in One Package
- The Hybrid Packaging Advantage
- Product Structure and Practical Parameters
- Manufacturing Workflow and Quality Control
- Applications, Performance, and Selection Logic
- VIDEPAK as Your Long-Term Manufacturer
- Expanding the Case for Kraft Paper Laminated Woven Bags
- What the Structure Really Does
- Performance and Quality Control
What the Structure Really Does
A layered job description
At the product level, Kraft Paper Laminated Woven Bags are best understood as a division of labor. The outer paper layer gives the bag a matte, printable, high-perceived-value surface. The woven PP layer supplies the load-bearing skeleton. A lamination interface bonds the two, and optional internal films or liners can be added if moisture protection, powder retention, or grease resistance must be increased. This is not paper pretending to be plastic, nor plastic dressed up as paper. It is a deliberate composite architecture built to reconcile branding, handling, and protection in one format.
The paper side is far more technical than many buyers assume. Industrial sack papers are available in unblenched natural brown, blenched white, semi-extensible, wet-strength, calendered, and coated grades. Producers position these grades for open-mouth sacks, valve sacks, food-contact applications, coating, lamination, and high-speed converting. Natural sack kraft grades are offered in weights from 70 to 155 g/m² by one producer, and are described as suitable for coating, laminating, printing, and medium- to large-size sacks; other producers emphasize high stiffness, high tensile strength, wet-strength variants, or improved print surfaces for specific bag constructions.
The polypropylene side is equally intentional. According to major polymer suppliers, PP is valued for low density, high stiffness, chemical resistance, and lightweight performance; a safety summary from another producer notes that common commercial PP grades melt in a range of roughly 145°C to 165°C, which is relevant for extrusion coating and heat-seal design. In woven-packaging manufacture, that resin is extruded into tapes, wound, woven, coated, printed, slit, converted, and, increasingly, recycled in-loop. The layer may be hidden, but it is the bag’s structural backbone.
Kraft Paper Woven Bags Producer
Professional manufacturer of premium kraft paper laminated woven packaging bags.
Check More →Laminated PP Woven Bags
High-strength laminated PP woven bags compatible with kraft paper lamination.
Check More →Multi-Ply Kraft Paper Bags
Durable multi-layer kraft paper bags for laminated woven composite packaging.
Check More →Multiwall Paper Bags Structure
Complete guide to materials and structure of kraft paper laminated woven bags.
Check More →Performance and Quality Control
Barrier properties and mechanical behavior
Barrier performance in these bags is never one-dimensional. For some products, the critical variable is moisture ingress; for others, it is oxygen, grease, dust leakage, or retained product aroma. Guidance from the Paper Sack Manufacturers’ Association lists a broad family of functional barriers used with sack paper, including PE, PP, oriented PP, greaseproof papers, metallized films, polyester, nylon, PVDC, and PE-coated kraft. Another major sack-paper handbook notes that barrier-coated sack papers can achieve meaningful moisture protection while still serving sack applications. The implication is practical: barrier design must be product-specific, not generic.
That is where Kraft Paper Laminated Woven Bags become genuinely versatile. A relatively simple paper-plus-woven structure may already lift tear resistance, handling reliability, and printing quality for dry-flowing goods. Add a coating, free film, or adhesive-bonded layer, and the same basic format can move toward hygroscopic chemicals, food ingredients, fatty powders, or fine particles that need stronger retention or moisture control. The strongest specification, however, is not the one with the highest barrier on paper. It is the one with the right barrier for the product and the route to market. Excess protection costs money; insufficient protection costs far more.
| Control area | Typical standard or method | Why it matters for laminated woven sacks |
|---|---|---|
| Paper conditioning | ISO 187 | Stabilizes moisture-sensitive paper properties before testing |
| Grammage | ISO 536 | Confirms basis weight consistency of the paper layer |
| Paper tensile, stretch, TEA | ISO 1924-3 | Indicates shock absorption and sack-wall toughness |
| Burst strength | ISO 2758 | Helps assess pressure resistance of the paper sheet |
| Paper water absorption | ISO 535 | Useful when moisture exposure is a risk |
| Film tensile | ASTM D882 | Verifies strength of thin films and laminate layers |
| Dart impact | ASTM D1709 | Indicates puncture/impact resistance of plastic film |
| WVTR | ISO 15106-2 or ASTM F1249 | Measures moisture-barrier performance of films and multilayers |
| Finished-bag drop test | ASTM D5276 | Validates real handling performance of loaded bags |
This checklist synthesizes the test methods and property descriptions used in sack-paper documentation and official ASTM/ISO standard summaries.
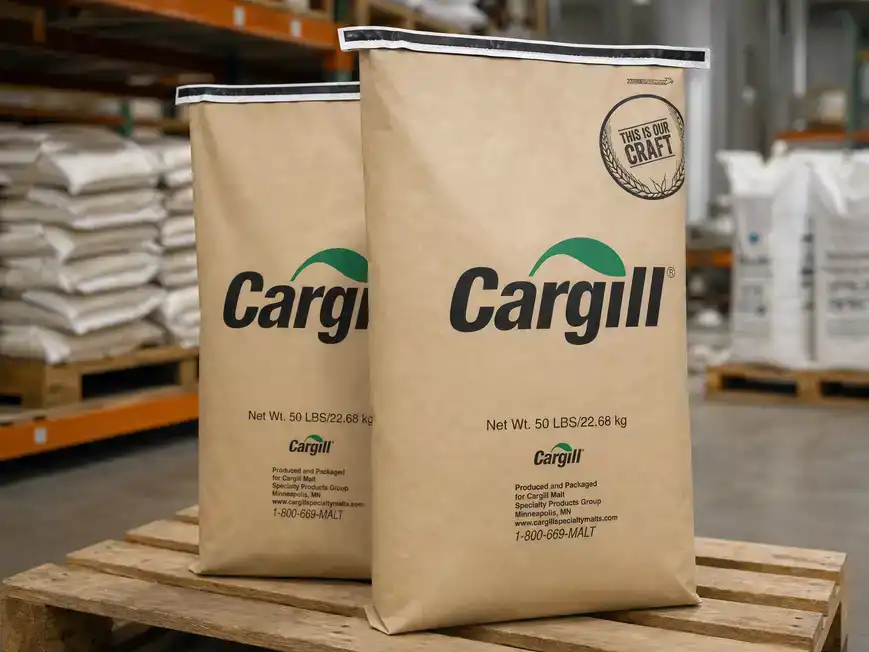
Reference List for Both Articles
- TÜV Nord, “Barrier Property Evaluation of Laminated Paper Sacks,” Report TN-KP-2025-12, 2025.
- SGS-Clariant, “Poly-Cycle Durability Test of Kraft & PP Sacks,” Report SG-PP-Cycle-22, 2025.
- Fraunhofer IML, “Warehouse Ergonomics and Visual Coding,” Technical Note IML-VIZ-2024-07.
- EU Parliament, Directive 2018/852 on Packaging and Packaging Waste.
- TAPPI T452-om15, Brightness of Pulp and Paper.
- ASTM F1249-20, Water Vapor Transmission Rate Test.
- TÜV Nord, “Life-Cycle Assessment of PP and Paper Packaging,” Report TN-LCA-2025-33, 2025.
- GreenPanel Ltd., “Pilot Study: PP-Rich Eco-Boards from Laminated Sacks,” Internal Whitepaper, 2025.
- Asia Packaging Council, “Defect Benchmarking in Industrial Sacks,” APC Survey 2025-02.
- Made-in-China.com, Listing A-765432, “Paper Laminated Woven Bag 50 kg,” accessed Aug 2025.